사이트맵 ×

토탈산업
현대보테코

Technology & solutions

엠쓰리파트너스
hnp인터프라
휴먼텍
한국마쓰이
기사제목
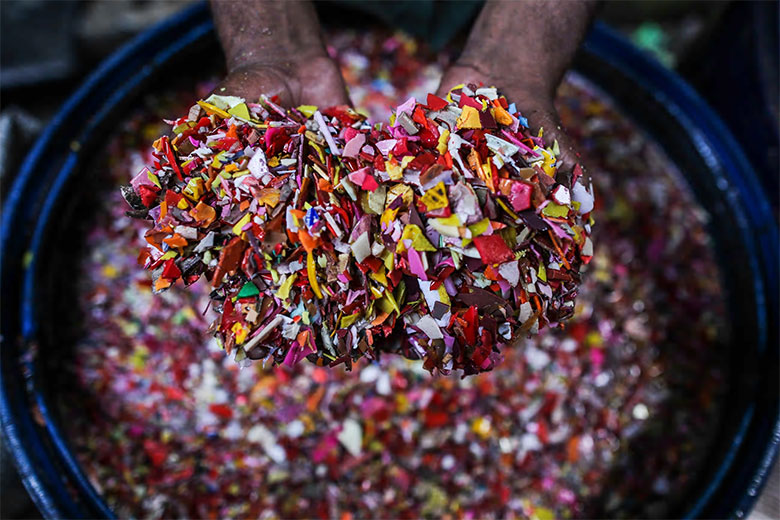
 Startups are turning plastic waste in developing countries into filament for 3D printers while employing local waste pickers   A worker washes shredded plastic waste for recycling. Photograph: Dhiraj Singh/Bloomberg via Getty  7 November 2016When Sidhant Pai visited a local rubbish dump in his home city of Pune, India, he was struck by the size and intensity of the operation. Large black crows swooping overhead, roaming pigs, overwhelming odours and groups of waste pickers collecting plastic bottles in large white sacks.   There are an estimated 15 million people globally who currently make their living from waste picking and many earn less than a dollar a day. A key problem, says environmental engineer Pai, is that workers only capture a tiny proportion of the value of the waste they collect, separate and transport to scrap dealers.   Together with his parents, Suchismita and Jayant Pai, he founded social enterprise Protoprint in 2012, one of a number of organisations trying to address the twin issues of poor conditions for waste pickers and plastic waste pollution. More than 300m tonnes of plastic are produced globally every year, with much ending up in the ocean (one refuse truck’s worth every minute), in landfill, or on city streets.  “Our focus was on looking into different ways to add value to the waste, we were agnostic about the specific product,” Pai says. After experimenting with making a few different products, Protoprint settled on making the plastic filament – the “ink” –­ for 3D printers. “It added a tremendous amount of value to the waste plastic while still being relatively simple to manufacture at the dump.”   Protoprint partnered with SWaCH, a Pune-based cooperative wholly owned by waste pickers. Together they have set up a low-cost filament production facility at a local rubbish dump in Pune operated by SWaCH waste pickers to convert plastic waste – specifically high-density polyethylene (HPDE) mostly used for plastic bottles – into 3D printing filament to eventually be sold to Indian or international 3D printing companies.   Protoprint waste pickers. Photograph: Protoprint Protoprint buys filament from SwaCH for 300 rupees (£3.50) per kg – if waste pickers sold the plastic waste directly to scrap merchants the pickers would receive around 19 rupees (23p) per kg, says Pai. “After factoring in the costs of production and the various other expenses, there is still a six to eight times multiplier per kilogram of filament,” he says.   The market for filament, the majority of which is made from virgin plastic, is growing rapidly. A report by a leading markets analyst predicted the 3D printing materials market would grow by nearly 266% over the next five years, to be worth £1.07bn by 2021.   However, most of it is expensive because of production and export costs, says William Hoyle, CEO of TechforTrade. The British charity is working to promote and standardise an ethical way for filament to be made from the plastic collected by waste collectors.    Ethical filament will be cheaper to buy than commercial filament, Hoyle says, because waste plastic is free resource and production costs are lower in developing countries.  “The ethical filament standard is an open standard,” says Hoyle. “We see the certification process happening in two ways. First, the social, environmental and economic assessment would be done by the waste collection organisation ... Second, the technical quality standard will be assessed by an independent third party and we are in discussion with a specialist assessor that will undertake this task.”   Amsterdam-based ReFlow, a social enterprise based in the Netherlands, works with one of TechforTrade’s printing partners in Tanzania, STICLab, on a pilot project in Dar es Salaam.   Co-founder Jasper Middendorp compares the potential of 3D printing to the development of mobile banking or solar in Africa, both of which flourished because infrastructure was broken.   “Tanzania is highly import dependent and has very little of its own production infrastructure,” he says, and 3D printing decentralises production without a huge capital expense or a great deal of specialised knowledge. This, he says, helps “make countries more self-sufficient instead of importing products from abroad that may not be suited to the local context”.   Previously supported by seed funding and the founders’ own money, ReFlow has just closed off a Kickstarter campaign, raising €26,000 (£23,000) and plans to launch the product in Amsterdam in February 2017. However, it is still working on quality control. “We haven’t produced market quality filament yet,” says Middendorp, “but we are hoping to do so within a month.”   The quality of the filament made from recycled waste plastic is a challenge for the whole 3D printing industry, says Pai. Protoprint’s pilot unit is currently making filament but is not yet ready to sell to market as there are problems with warping. The company is working with a team of senior polymer scientists from the National Chemical Laboratory to develop an additive for the filament to prevent the warping issue, funded by a government grant.   Protoprint says it currently has 4,000kg of pre-orders, mostly from small- and medium-sized distributors based in the US, UK, Germany and India looking to sample and test the filament. “We have not yet started commercial operations and are working on improving our filament quality before we do so,” says Pai.   Quality is not necessarily an insurmountable issue, says Thomas Birtchnell, a lecturer at the University of Wollongong and author of 3D Printing for Development in the Global South. Much of the recycled filament is destined for “the open source market for low-end products,” he says, “they may not look glamorous but they are still functional products that can be used in development contexts”.   The greatest potential 3D printing offers the developing world is not for the products made, but for “putting the means of production into the hands of the local people”, says Jeremy Faludi, a sustainable design strategy consultant and teacher at the Minneapolis College of Art and Design. The market for ethical filament is a small one, he adds, but “if the quality can match virgin filament at a similar price point, then it can be a large market. As with all things in sustainability, customers like the story, they’re just not willing to pay more for it.”    https://www.theguardian.com/sustainable-business/2016/nov/06/3d-printing-plastic-waste-poverty-development-protoprint-reflow-techfortrade  
jennifer 2016-11-16
기사제목
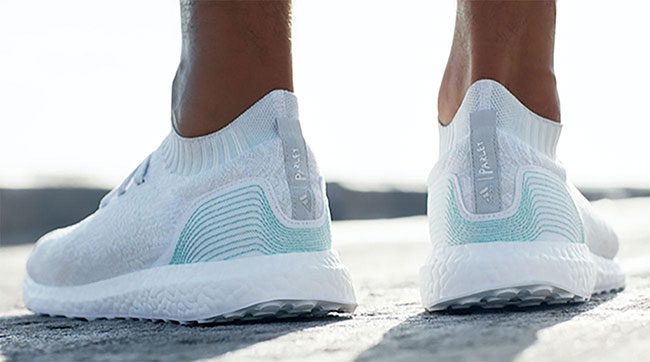
Mark J. BurnsMonday November 7th, 2016 Parley for the Oceans and adidas have unveiled new performance products this week with the aim of increasing awareness about ocean plastic pollution. The new products include the UltraBOOST Uncaged Parley running shoe along with soccer jerseys for Real Madrid and Bayern Munich, who will sport them later this month. Both products are the first apparel and footwear produced with Parley ocean plastic and waste recovered from the coastal areas of the Maldives. In honor of World Oceans day this summer, they also created a limited edition adidas x Parley shoe created from ocean waste. “This represents another step on the journey of adidas and Parley for the Oceans. We have not only managed to make footwear from recycled ocean plastic, but have also created the first jersey coming 100 percent out of the ocean,” said Eric Liedtke, adidas group executive board member responsible for global brands, in a statement. adidas will manufacture 7,000 pairs of the UltraBOOST Uncaged Parley, a shoe that is created with 95% ocean plastic. The running footwear is part of adidas’s commitment to creating one million pairs of UltraBOOST made with Parley ocean plastic by next year’s end. “At this point, it’s no longer just about raising awareness. It’s about taking action and implementing strategies that can end the cycle of plastic pollution for good,” said Cyrill Gutsch, Founder, Parley for the Oceans in a statement. “Eco-innovation is an open playing field. With the release of the Ocean Plastic jerseys and UltraBOOST Uncaged adidas x Parley shoes, we’re inviting every consumer, player, team and fan to own their impact under Parley A.I.R. and define their role within the movement.” http://www.si.com/tech-media/2016/11/07/adidas-parley-ocean-plastic-pollution#
Ms.Kang 2016-11-09
기사제목
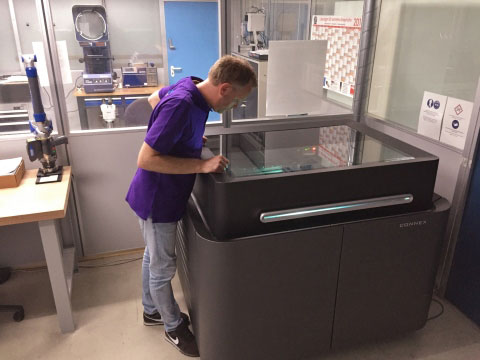
Dutch Manufacturer PromoldingReduces Injection Mold Lead Times By 93%Thanks to Stratasys 3D Printing Technology3dprint.comby Joseph Young | Oct 27, 2016Multi-billion dollar 3D printing and additive manufacturing solutions company Stratasys, in cooperation with Dutch manufacturer Promolding, has successfully reduced injection mold lead times by 93% through the utilization of Stratasys PolyJet 3D printing solutions. Injection molding, one of the most widely used manufacturing processes, is often leveraged by manufacturers with massive volumes of products to create plastic items such as chairs and toys.ProMolding_PRIM_sensor_housingIn an injection molding process, a polymer or plastic material is heated up to liquid form until it becomes flexible enough to fit in any shape of a mold. The liquefied polymer is then injected into a custom mold using pressure, and the entire process can be completed relatively quickly, unlike many other manufacturing methods.In most cases, the polymer injection phase, which seems ostensibly complex and sophisticated, is simple and swift, while the creation of the mold requires weeks of preparation. Jeroen Gross, Product Development Manager at Promolding, an industry leader in the global design, engineering and manufacturing of high-tech plastic parts and components, noted that the development of injection molds normally takes manufacturers around six weeks. However, with accurate and efficient 3D printing of molds, Gross explained that the mold creation phase can be reduced by 93%, which allows Promolding to complete the majority of the injection molding manufacturing process within just a few days.“Traditionally, injection mold development required at least a six-week lead time,” said Gross. “By designing and 3D printing the molds in-house, we can produce molds in just three days.”Due to the efficiency of Stratasys PolyJet solutions in designing and developing molds, Gross stated that his team came to a consensus to rely on Stratasys rather than other commercial 3D printers in the market.“We became increasingly aware of the need for a 3D printer that would help us optimize our product development process,” he said. “We looked at several different options, but fell in love with Stratasys’ Objet Connex 3D Printer and its ability to not only improve our prototyping, but also become a key driver for our PRIM (3D Printed Injection Molding division) business.”“PRIM is available to our customers as an additional service in parallel to prototyping and traditional injection molding,” he continued. “In the future, we believe PRIM will be seen as a commonplace process of its own. We have come a long way and we’ll continue to explore further applications in which PolyJet 3D printing can enhance our offering.”Recently, Promolding designed a fiber optic sensor house for their client Fugro, a global leader in integrated geotechnical, subsea, survey and geoscience services. The extremely complex part needed to be completed in a short amount of time, and with traditional injection molding, the deadline may have been close to impossible to meet. By using the Objet500 Connex 3D printer, however, Promolding was able to quickly produce a series of molds, which in turn allowed Fugro to create over 50 samples of the product housing in different materials including PP, TPE and PBT.“Particularly with the development of bigger and more complex products, it is crucial as a business that we are as efficient as possible throughout the product development process, without compromising on quality,” said Gross. “Having our 3D printer has enabled us to achieve this and given us an incredible level of flexibility. We can use the technology in the early development phases to speed up the design process and develop, review and adapt prototypes earlier, but also extend the efficiencies into production through our PRIM process. It really has been a game-changer and we’ve seen the benefits passed onto our customers.”Promolding’s major clients include Heineken and Airbus, the latter being one of the biggest pioneers of 3D printing in the aerospace industry. The company had been using the Objet500 Connex printer for several other product development applications, but they’ve only just begun to use it to create injection molds, combining two major manufacturing technologies and potentially creating new business opportunities.“Additive manufacturing has the power to transform business models and Promolding is a prime example,” said Andy Middleton, General Manager of Stratasys EMEA. “We are seeing more and more customers realize the full potential of our PolyJet 3D printing technology, going beyond the immediate efficiencies within product design and pioneering the disruption of traditional manufacturing processes. In the case of injection molding, 3D printed injection molds are redefining the price-performance benchmark for low volume production, giving manufacturers the flexibility to produce products in the final injected material faster than ever before.”https://3dprint.com/153744/stratasys-promolding-injection/
Ms.Kang 2016-10-31
기사제목
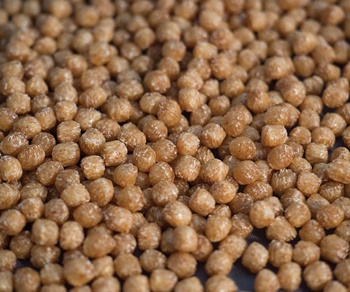
TIPS AND TECHNIQUESBy: Michael Parker from Green DotFrom: Plastics TechnologyIssue: September 2016Originally targeted mainly for extrusion, new options for wood-plastic composites have been optimized to open doors for injection molding applications.  For molding WPCs, the ideal pellet should be about the size of a small BBand rounded to achieve an optimal surface-to-volume ratio.While wood-plastic composites (WPCs) broke onto the scene in the 1990s as materials primarily extruded into boards for decking and fencing, optimization of these materials for injection molding since then has greatly diversified their potential applications as durable and sustainable materials. Environmental friendliness is an attractive feature of WPCs. They come with a significantly lower carbon footprint than purely petroleum-based materials and can be formulated using exclusively reclaimed wood fibers.A wider range of material options for WPC formulations is opening new opportunities for molders. Recycled and biodegradable plastic feedstocks can further enhance the sustainability of these materials. There are an increasing number of aesthetic options, which can be manipulated by varying the wood species and wood particle size in the composite. In short, optimization for injection molding and the growing list of options available to compounders mean WPCs are a much more versatile material than was once thought.WHAT MOLDER SHOULD EXPECT FROM SUPPLIERS A growing number of compounders are now offering WPCs in pellet form. Injection molders should be discerning when it comes to expectations from compounders in two areas especially: pellet size and moisture content.Unlike when extruding WPCs for decking and fencing, uniform pellet size for even melting is crucial in molding. Since extruders do not have to worry about filling their WPC into a mold, the need for uniform pellet size is not as great. Hence, it’s important to verify that a compounder has the needs of injection molders in mind, and is not overly focused on the earliest and initially most prevalent uses for WPCs.When pellets are too large they have a tendency to melt unevenly, create additional friction, and result in a structurally inferior final product. The ideal pellet should be about the size of a small BB and rounded to achieve an ideal surface-to-volume ratio. These dimensions facilitate drying and help to ensure a smooth flow throughout the production process. Injection molders working with WPCs should expect the same shape and uniformity they associate with traditional plastic pellets.Dryness is also an important quality to expect from a compounder’s WPC pellets. Moisture levels in WPCs will increase along with the amount of wood filler in the composite. While both extruding and injection molding require low moisture content for best results, recommended moisture levels are slightly lower for injection molding than for extrusion. So again, it’s important to verify that a compounder has considered injection molders during manufacturing. For injection molding, moisture levels should be below 1% for optimal results.When suppliers take it upon themselves to deliver a product already containing acceptable levels of moisture, injection molders spend less time drying the pellets themselves, which can lead to substantial savings of time and money. Injection molders should consider shopping around for WPC pellets shipped by the manufacturer with moisture levels already below 1%.FORMULA & TOOLING CONSIDERATIONS The ratio of wood to plastic in the formula of a WPC will have some effect on its behavior as it goes through the production process. The percentage of wood present in the composite will have an effect on the melt-flow index (MFI), for example. As a rule, the more wood that is added to the composite, the lower the MFI.The percentage of wood will also have a bearing on the strength and stiffness of the product. Generally speaking, the more wood that’s added, the stiffer the product becomes. Wood can make up as much as 70% of the total wood-plastic composite, but the resulting stiffness comes at the expense of the ductility of the final product, to the point where it may even risk becoming brittle.Higher concentrations of wood also shorten machine cycle times by adding an element of dimensional stability to the wood-plastic composite as it cools in the mold. This structural reinforcement allows the plastic to be removed at a higher temperature where conventional plastics are still too soft to be removed from their molds.If the product will be manufactured using existing tools, the gate size and general shape of the mold should factor into the discussion of optimal wood-particle size. A smaller particle will likely better serve tooling with small gates and narrow extensions. If other factors have already led designers to settle on a larger wood particle size, then it may be beneficial to redesign the existing tooling accordingly. But, given the existing options for different particle sizes, this outcome should be completely avoidable.PROCESSING WPCs Processing specifics also have a tendency to fluctuate significantly based on the final formulation of the WPC pellets. While much of processing remains similar to that of traditional plastics, specific wood-to-plastic ratios and other additives meant to achieve some desired look, feel, or performance characteristic may need to be accounted for in processing. WPCs are also compatible with foaming agents, for example. Addition of these foaming agents can create a balsa-like material. This is a useful property when the finished product needs to be especially lightweight or buoyant. For the purpose of the injection molder, though, this is yet another example of how the diversifying composition of wood-plastic composites may lead to there being more to consider than when these materials first came to market.Processing temperatures are one area where WPCs differ significantly from conventional plastics. WPCs generally process at temperatures around 50° F lower than the same unfilled material. Most wood additives will begin to burn at around 400 F.Shearing is one of the most common issues to arise when processing WPCs. When pushing a material that’s too hot through too small a gate, the increased friction has a tendency to burn the wood and leads to telltale streaking and can ultimately degrade the plastic. This problem can be avoided by running WPCs at a lower temperature, ensuring the gate size is adequate, and removing any unnecessary turns or right angles along the processing pathway.Relatively low processing temperatures mean that manufacturers seldom need to achieve temperatures higher than for a traditional polypropylene. This minimizes the difficult task of taking heat out of the manufacturing process. There’s no need for the addition of mechanical cooling equipment, molds specifically designed to reduce heat, or other extraordinary measures. This means further reduced cycle times for manufacturers, on top of already faster cycle times due to the presence of organic fillers.  New molding applications for WPCs include this toy boat.  NOT JUST FOR DECKING WPCs aren’t just for decking anymore. They are being optimized for injection molding, which is opening them up to a vast array of new product applications, from lawn furniture to pet toys. The wide range of formulations now available can enhance the benefits of these materials in terms of sustainability, aesthetic diversity, and features such as buoyancy or rigidity. Demand for these materials will only increase as these benefits become better known.For injection molders, this means a number of variables specific to each formulation must be accounted for. But it also means molders should expect a product that’s better suited to injection molding than feedstock that was designated primarily to be extruded into boards. As these materials continue to develop, injection molders should raise their standards for the characteristics they expect to see in the composite materials delivered by their suppliers.   http://www.ptonline.com/articles/what-you-should-know-about-molding-wood-plastic-composites
Ms. Kang 2016-08-30
기사제목
 August 23, 2016Plastics News Report Philadelphia-The future of food packaging may be dairy, dairy clear.Researchers with the U.S. Department of Agriculture are developing a food packaging film made from the milk protein casein that is bio-based, biodegradable and edible.  Research leader Peggy Tomasula said the protein-based films are oxygen blockers that help prevent food spoilage, which would help to reduce food waste, and is up to 500 times more effective than currently traditional films. And at the same time, the film itself does not clog up the waste stream.  Or, users could just eat the film along with the food.  “We are currently testing applications such as single-serve, edible food wrappers,” said study co-leader Laetitia Bonnaillie. “For instance, individually wrapped cheese sticks use a large proportion of plastic — we would like to change that.”  Early studies produced a film that was difficult to handle and dissolved in water too easily. Researchers made improvements by adding citrus pectin.  Existing biodegradable films on the market made of starch are more porous, allowing oxygen through microholes, the researchers said in an Aug. 21 news release.  Because the film can be dissolved in water, there also is potential to use it to wrap single-serve items such as coffee or soups, with individual packets dropped into boiling water, disposing of the packaging at the same time as heating up the food.  In addition, the protein can be made into a coating that could be sprayed onto food such as cereal flakes, which are currently coated with sugar to keep them crunchy in milk, the researchers said.  Individual food packets using the milk protein would still need to be packaged in cardboard or larger plastic packages to prevent them from dissolving if they got wet.  The Department of Agriculture scientists presented their research at a meeting of the American Chemical Society in Philadelphia Aug. 22.http://www.plasticsnews.com/article/20160823/NEWS/160829946/researchers-have-a-new-whey-to-make-film
Ms. Kang 2016-08-30